How this product class behaves
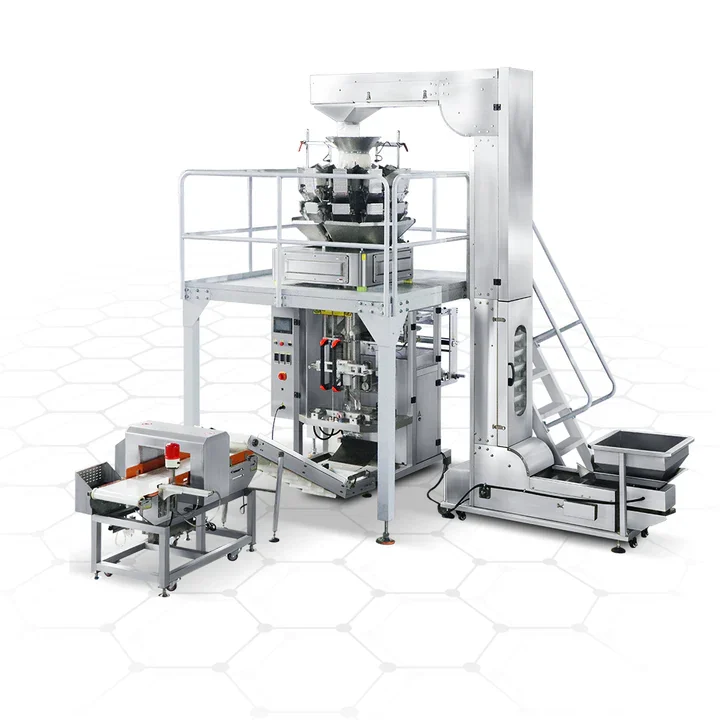
The typical process uses auger filler, vacuum doser or loss-in-weight dosing system supplied through a covered hopper with controlled replenishment and optional agitation. The equipment should be configured to test bulk density variation, deaeration, dust extraction and refill effects.
Before discussing speed or automation, define the actual operating window: minimum and maximum dose, product temperature, density, viscosity or bulk density, inclusions, foam, shear sensitivity, corrosivity, pack dimensions and closure. A single nominal sample is not enough for a robust specification.
Recommended filling technologies
Primary route
Auger filler, vacuum doser or loss-in-weight dosing system.
Product supply
A covered hopper with controlled replenishment and optional agitation.
Critical control
Test bulk density variation, deaeration, dust extraction and refill effects.
Temperature and product condition
Normally ambient with humidity controlled where the powder is hygroscopic. Temperature changes may alter viscosity, foam, gas breakout, dose accuracy, closure performance or pack stability. Define where temperature is measured and the permitted deviation.
Cleaning, changeover and material compatibility
Plan for accessible hoppers and tooling, dust containment and a validated allergen/changeover plan. Product-contact materials, elastomers, lubricants, surface finish and drainage should be reviewed against every formulation. Include safe access, line clearance, product recovery and waste handling.
Principal production risks
Risk focus
Dust exposure, segregation, bridging, static, poor seals and variable settled volume. The process and machinery risk assessments should cover normal running, refill, sampling, adjustment, blockage clearance, cleaning and maintenance.
What to prove in a product trial
- Repeatable dose at minimum and maximum line speed
- Clean cut-off and acceptable pack presentation
- Stable product feed through refilling and batch end
- Changeover and cleaning time using the intended method
- Closure, label, code and distribution performance after filling
Example product applications
Cocoa Hazelnut Filling in Jars and Tubs
Powder
Bakery & confectionery ingredientsCocoa Hazelnut Filling in Stand-up Pouches
Powder
Bakery & confectionery ingredientsCocoa Hazelnut Filling in Single-dose Sachets
Powder
Bakery & confectionery ingredientsCocoa Hazelnut Filling in Retail Bags
Powder
Bakery & confectionery ingredientsCocoa Hazelnut Filling in Bulk Sacks
Powder
Dry foods & ingredientsFlour in Jars and Tubs
Powder
Dry foods & ingredientsFlour in Stand-up Pouches
Powder
Dry foods & ingredientsFlour in Single-dose Sachets
Powder
Dry foods & ingredientsFlour in Retail Bags
Powder
Dry foods & ingredientsFlour in Bulk Sacks
Powder
Dry foods & ingredientsCornflour in Jars and Tubs
Powder
Dry foods & ingredientsCornflour in Stand-up Pouches
Powder
Common questions
Which filling machine suits a powder?
A auger filler, vacuum doser or loss-in-weight dosing system is the normal starting point. Final selection depends on dose, accuracy, product feed, temperature, pack, cleaning, contact materials and required output.
Why are product samples needed before specifying a filler?
Published viscosity or density values do not show aeration, particles, stringing, shear sensitivity, temperature effects or interaction with the nozzle and pack. A representative test exposes these issues before manufacture.
Can one machine cover several product viscosities or formats?
Often yes, within a defined operating window. The specification should identify the easiest and most difficult products, smallest and largest doses, every pack height and diameter, and the acceptable changeover method.
How is filling accuracy confirmed?
Agree whether the target is volume or mass, the permitted tolerance, test method and sampling frequency. Measure warm-up, hopper refill, speed changes and end-of-batch conditions rather than only stable running.
What determines the real line speed?
The slowest repeatable operation governs output. Product refill, container loading, filling time, closure handling, label application, rejects, accumulation, cleaning and operator intervention all affect the sustainable rate.