A practical production route
Use the eight stages below to compare the complete route for your product, from preparation and pack handling through to dispatch. For anti-seize paste, the critical issues are product tails, air pockets, inconsistent dose weight and smearing around the neck.
Define the product window
Measure the production range for anti-seize paste: fill volume or weight, density, viscosity or flowability, temperature, largest inclusion, foam, chemistry and shelf-life process. Select equipment against the worst case, not the easiest sample.
Prepare and feed consistently
Prepare anti-seize paste to a repeatable specification and supply the filler through a hopper or short, large-bore transfer route that avoids excessive restriction. Control batch-to-batch variation and avoid long, restrictive or difficult-to-clean pipework.
Apply the required treatment
Mix anti-seize paste without entraining excess air. Define a stable temperature and resting time before filling so viscosity and dose behaviour remain repeatable.
Prepare the empty pack
Inspect and present pots and tubs consistently, using guides or tooling that protects the pack finish and confirms presence before filling.
Fill accurately and cleanly
Use a piston, servo-piston, progressive-cavity or positive-displacement filler. Manage stringing with shut-off nozzles and match acceleration to viscosity. Set the nozzle and container handling so the outside of the pots and tubs remains clean for closing and labelling.
Close or seal the pack
Apply snap-on lids or heat-sealed foils with repeatable torque or force. Include cap/closure presence detection and a routine check of opening performance, leakage and tamper evidence.
Label, code and verify
Choose a label, sleeve or direct-print method that suits the surface, shape and handling of the pots and tubs. Verify the code remains legible through distribution and use.
Inspect and pack for distribution
Check fill quantity, pack integrity, code and presentation before accumulating or case packing. Confirm the finished pots and tubs survives handling, sleeve wrapping, case packing, palletisation and transport.
Equipment options for anti-seize paste
These machine types provide an initial route. Dose range, contact materials, output, utilities, change parts and controls should be agreed after a representative product and pack trial.
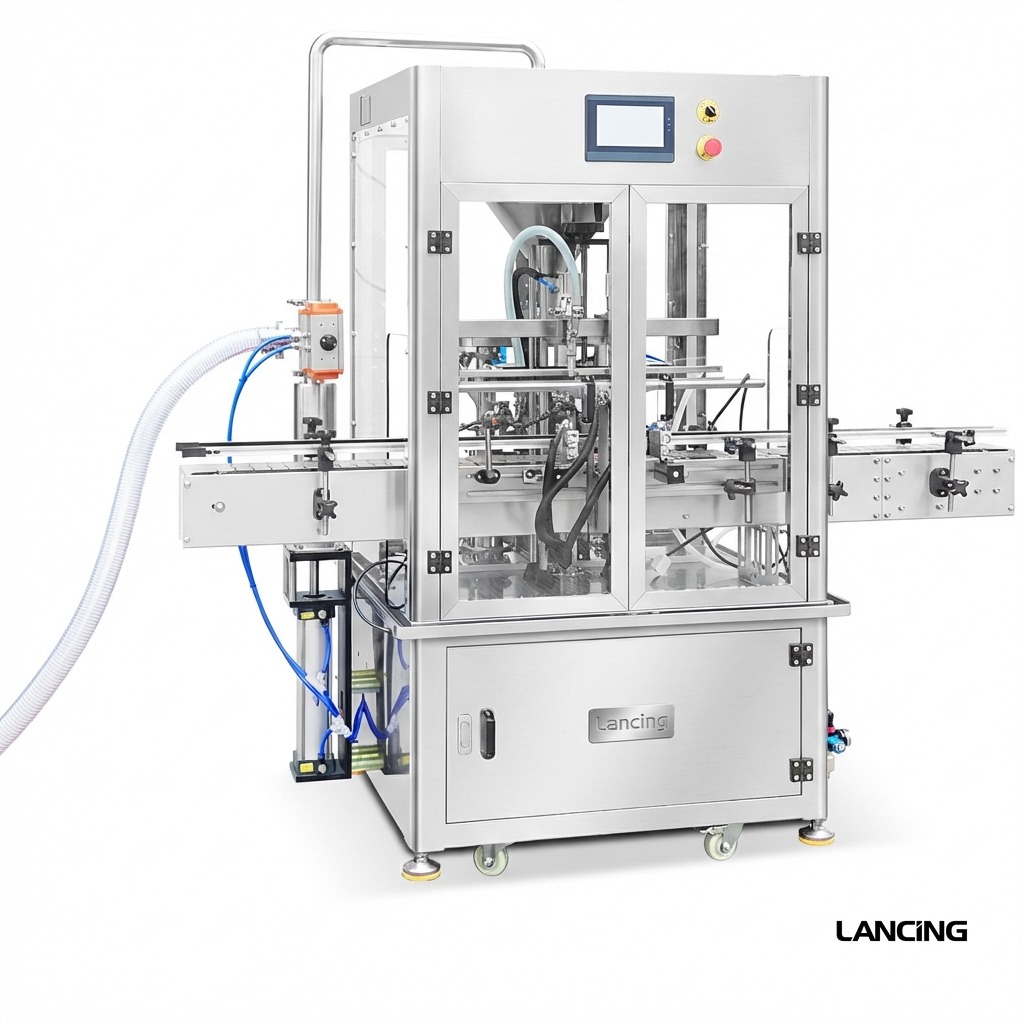 Recommended filling route
Automatic servo piston filling machine
A practical starting point for anti-seize paste: piston, servo-piston, progressive-cavity or positive-displacement filler with product-specific contact parts and controls.
View Lancing solutions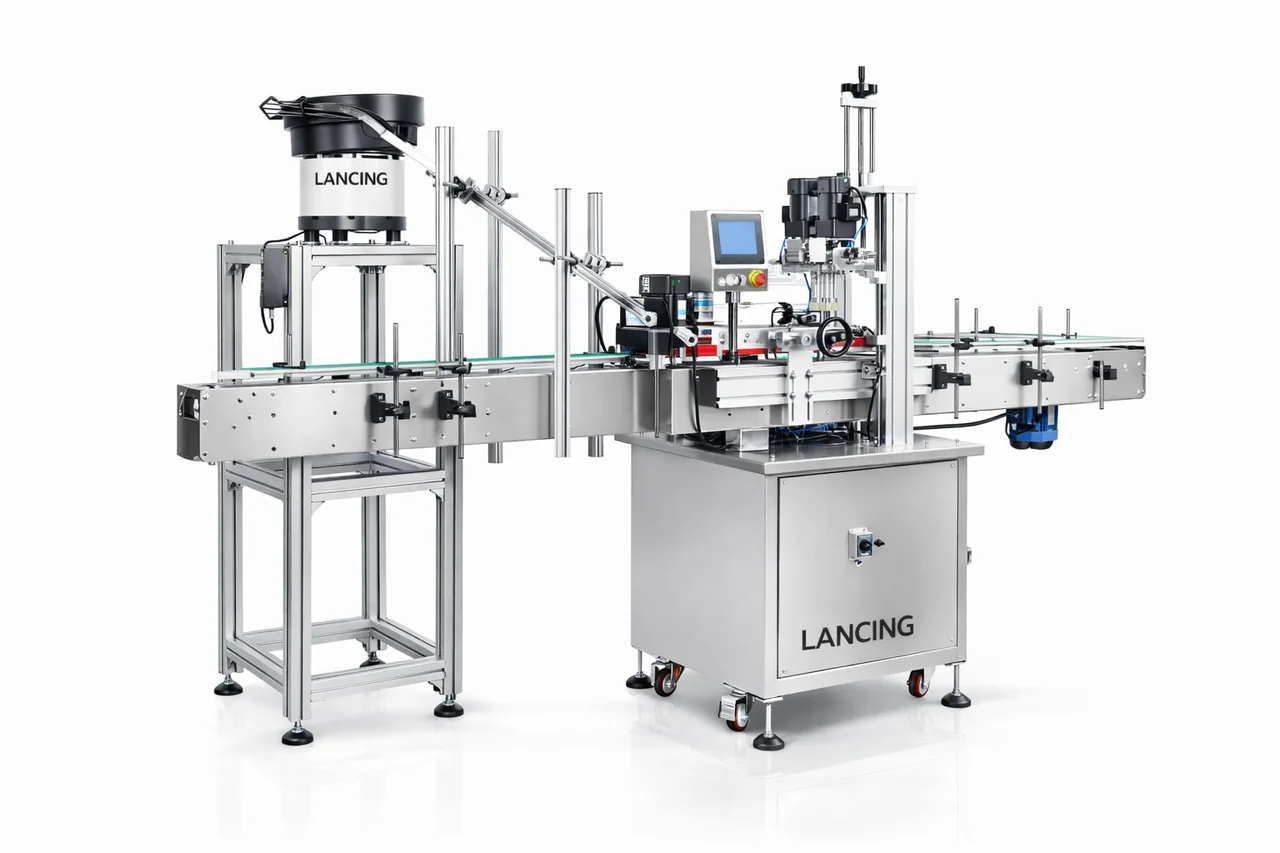 Closing and sealing
Automatic closure application
Apply and tighten snap-on lids or heat-sealed foils with controlled torque, force or position.
View Lancing solutions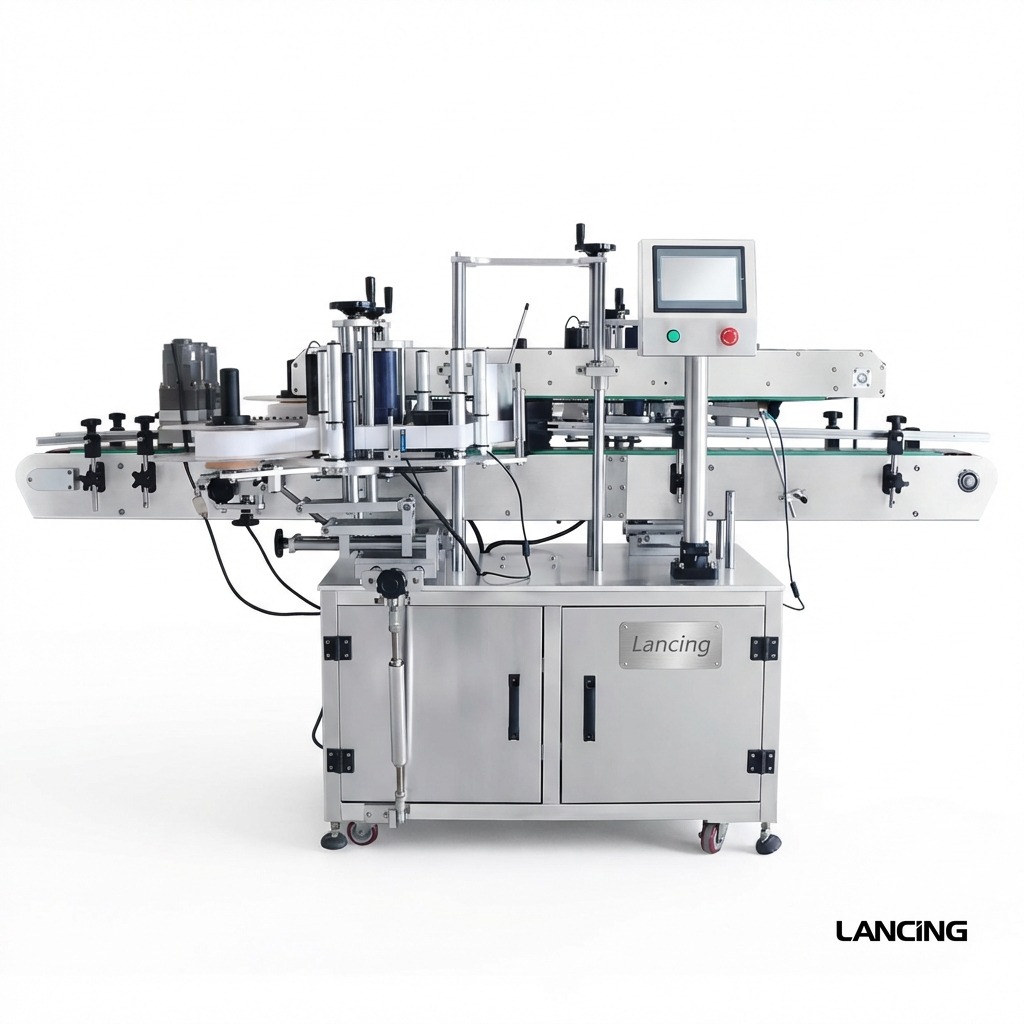 Labelling and coding
Automatic labelling system
Apply labels and traceability data to pots and tubs, with inspection where mix-up risk justifies it.
View Lancing solutionsEngineering, safety and quality controls
Product behaviour
Test viscosity, density, foaming, particle size or flowability using production-representative anti-seize paste. Manage stringing with shut-off nozzles and match acceleration to viscosity.
Operator protection
Guard access to moving tooling and control exposure to anti-seize paste. Address product tails, air pockets, inconsistent dose weight and smearing around the neck in the machinery and process risk assessment.
Cleaning and changeover
Plan for quick-release product-contact parts or a validated clean-in-place arrangement. Confirm recovery, flushing, allergen or chemical segregation and safe disposal before purchase.
Pack validation
Run the actual pots and tubs and snap-on lids or heat-sealed foils through filling, closing, labelling and transit tests. Supplier drawings alone do not show real production variation.
Selecting equipment by weekly throughput
| Weekly volume | Typical equipment level | Planning approach |
|---|---|---|
| Under 500 | Desktop or manual-assist | Prioritise low changeover time, flexible tooling and safe repeatability. |
| 500–2,000 | Compact semi-automatic | Separate filler, closer and labeller can provide a practical step up without a full conveyor line. |
| 2,000–10,000 | Two-head or compact inline | Use controlled product feed, powered conveyors and automatic closing or labelling where labour is the constraint. |
| 10,000+ | Multi-head automatic line | Balance every station, include accumulation and specify inspection, rejection and end-of-line handling. |
Prove the line with your product and packaging
The most useful test uses the final anti-seize paste, pots and tubs, snap-on lids or heat-sealed foils, label and code. Include the most difficult size or formulation, not only the easiest product.
Discuss this applicationCommon questions about filling anti-seize paste
What filling machine is best for anti-seize paste?
A piston, servo-piston, progressive-cavity or positive-displacement filler is the usual starting point because anti-seize paste behaves as a smooth viscous product normally handled by piston, servo-piston, progressive-cavity or lobe-pump filling. The actual choice depends on dose, temperature, inclusions, required accuracy, cleaning regime and output.
Can anti-seize paste be filled into pots and tubs?
Yes, provided the pots and tubs, snap-on lids or heat-sealed foils and product are compatible. Test dimensional variation, fill temperature, headspace, leakage, closure performance, label adhesion and distribution before specifying the line.
Should anti-seize paste be filled hot or cold?
Anti-seize Paste is commonly handled with held within a defined range because viscosity changes with temperature. The final temperature must come from the validated formulation, preservation method, pack material and closure process.
How do you achieve a clean fill with anti-seize paste?
Use a positive shut-off nozzle, tune fill acceleration and position, and keep the pots and tubs stable. Product trials determine whether a piston, pump or gravity method gives the cleanest result.
How should pots and tubs be closed after filling anti-seize paste?
Apply snap-on lids or heat-sealed foils with repeatable torque or force. Include cap/closure presence detection and a routine check of opening performance, leakage and tamper evidence.
What output can a anti-seize paste filling line achieve?
Output depends on dose size, pack handling, fill time, closure method, cleaning and operator loading. As a planning guide: desktop equipment suits under 500 packs/week, compact systems 500–2,000, two-head lines 2,000–10,000 and multi-head systems 10,000+.
What samples are needed to test anti-seize paste?
Supply representative anti-seize paste, the complete pots and tubs, snap-on lids or heat-sealed foils, labels and any coding specification. Include the full product range, especially the highest viscosity, largest inclusion or most difficult pack size.